| Manufacturing Scope |
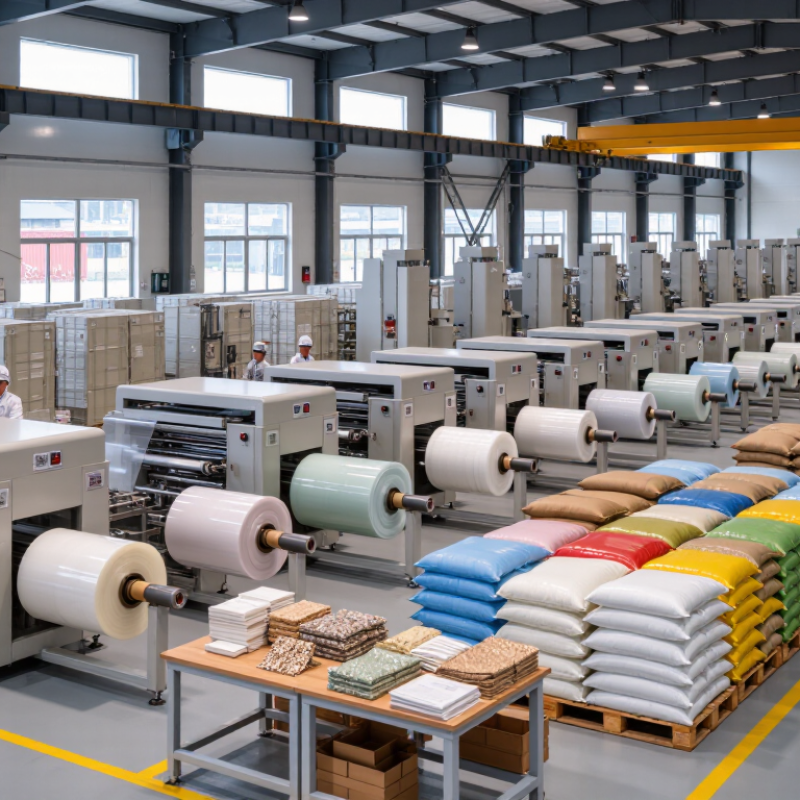
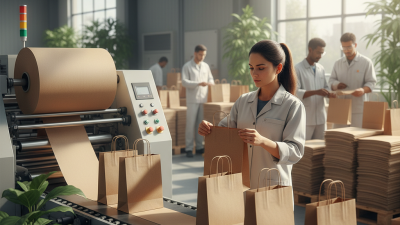
In-house or clearly controlled production for laminated pouches, stand-up bags, flat-bottom bags, woven sacks, paper bags, or other required formats. |
At least 2–3 bag structures or formats suitable for the buyer’s application. |
Factory capability statement, production-flow chart, equipment list, and recent product samples. |
A broad but relevant production scope reduces outsourcing risks and improves quality consistency. |
| Material Selection |
Materials matched to product sensitivity, filling method, storage conditions, and recycling requirements. |
Typical structures may include PE, PP, PET, BOPP, aluminum foil, paper, or multilayer films, depending on the application. |
Material specifications, technical data sheets, layer structure, thickness tolerance, and resin or paper origin information. |
Correct material selection affects barrier performance, seal strength, shelf life, and total packaging cost. |
| Barrier Performance |
Testing for oxygen transmission rate, water vapor transmission rate, light protection, and aroma retention when required. |
Performance targets should be defined by the product rather than selected only by bag appearance. |
Third-party or in-house test reports showing OTR, WVTR, and relevant test conditions. |
Barrier properties are critical for food, coffee, chemicals, pharmaceuticals, and moisture-sensitive products. |
| Printing Capability |
Rotogravure, flexographic, digital, or other printing processes with controlled color registration and repeatability. |
Confirm the number of colors, maximum print width, repeat length, artwork format, and color approval process. |
Color proof, approved pre-production sample, ink specifications, and print inspection records. |
Reliable color control protects brand consistency and reduces disputes over mass-production appearance. |
| Size and Thickness Control |
Documented control of bag dimensions, film thickness, gusset size, seal width, and finished weight. |
Require agreed tolerances in the purchase specification; common film thickness ranges vary by structure and use. |
Inspection plan, calibrated measuring equipment records, and sample dimensional report. |
Accurate dimensions improve filling-line performance, stacking stability, and shipping efficiency. |
| Sealing and Mechanical Strength |
Testing for heat-seal strength, tensile strength, puncture resistance, drop performance, and leak resistance where applicable. |
Performance limits should be confirmed through product-specific testing before bulk production. |
Seal-strength data, tensile or puncture test results, drop-test records, and approved samples. |
Strong seals and durable materials help prevent leakage, breakage, and product contamination. |
| Food-Contact Compliance |
Materials and inks suitable for the intended market and product-contact conditions when packaging food or beverages. |
Compliance may involve applicable requirements such as U.S. FDA food-contact rules, EU Framework Regulation (EC) No. 1935/2004, or China GB 4806 standards. |
Declaration of compliance, migration test reports, raw-material documentation, and traceability records. |
Requirements differ by destination market, food type, temperature, and contact duration. |
| Quality Management |
Formal procedures covering incoming materials, in-process checks, finished-goods inspection, nonconformance handling, and corrective action. |
An ISO 9001-certified system is useful, but actual inspection records should also be reviewed. |
Quality manual, ISO 9001 certificate if applicable, inspection forms, corrective-action reports, and audit results. |
A documented quality system makes production performance more repeatable and traceable. |
| Factory Audit Readiness |
Willingness to support remote or on-site audits and provide verifiable production and quality records. |
Factory identity, production address, ownership or operating status, and audit contact should be consistent across documents. |
Business license, factory address, audit checklist, production photos, and live video-tour access. |
Factory verification helps distinguish actual manufacturers from trading-only suppliers. |
| Minimum Order Quantity |
MOQ matched to printing method, material structure, bag size, and tooling requirements. |
Printed orders commonly require higher MOQs than plain or digitally printed bags; obtain a written quotation for each SKU. |
Formal quotation showing MOQ, tooling or cylinder charges, setup fees, and price breaks. |
Understanding MOQ prevents unexpected inventory, setup, and cash-flow costs. |
| Sample and Approval Process |
Pre-production samples, artwork confirmation, color approval, and signed specifications before mass production. |
Use a sealed approval sample or golden sample for dimensions, materials, printing, and functional testing. |
Sample approval form, artwork proof, technical specification, and change-control procedure. |
A documented approval process provides a clear reference for final inspection and claims. |
| Production Lead Time |
Lead-time planning that separates artwork approval, raw-material preparation, printing, bag making, inspection, and shipping. |
Typical timing varies by structure and order size; confirm a written schedule rather than relying on a general promise. |
Production schedule, capacity confirmation, delivery terms, and delay-notification procedure. |
Accurate planning helps global buyers coordinate inventory and vessel or air-freight bookings. |
| Traceability |
Lot or batch identification linking finished bags to materials, production dates, machines, operators, and inspection results. |
Every shipment should be traceable to a defined production lot and retained sample. |
Batch coding method, material certificates, production records, and retained-sample policy. |
Traceability supports recalls, root-cause analysis, and regulatory investigations. |
| Sustainability Options |
Material-reduction designs, recyclable mono-material options, recycled content where suitable, paper alternatives, and waste controls. |
Evaluate the complete structure and local recycling conditions instead of accepting unsupported “eco-friendly” claims. |
Material composition, recycled-content evidence, recyclability assessment, and environmental management records such as ISO 14001 if applicable. |
Sustainability claims must match the actual material structure and the destination market’s recycling infrastructure. |
| Export Experience |
Experience with international documentation, export packaging, carton marking, Incoterms, and destination-specific requirements. |
Confirm the supplier can support the buyer’s preferred Incoterm and destination port or airport. |
Commercial invoice sample, packing list, export documentation checklist, and shipping references with confidential details removed. |
Export competence reduces customs, labeling, and shipment-coordination problems. |
| Pre-Shipment Inspection |
Inspection of quantity, dimensions, appearance, printing, seals, packaging method, and carton markings before dispatch. |
Use an agreed sampling plan and acceptance criteria, such as an AQL-based inspection where appropriate. |
Pre-shipment inspection report, photos, carton count, pallet details, and test results. |
Final inspection provides an additional control point before goods leave China. |
| Commercial Transparency |
Clear pricing for materials, printing, tooling, testing, packing, freight terms, payment conditions, and revisions. |
Compare quotations using the same bag structure, thickness, quantity, delivery term, and quality requirements. |
Detailed quotation, sales contract, payment schedule, warranty terms, and complaint-resolution process. |
Transparent commercial terms make supplier comparisons more accurate and reduce hidden-cost disputes. |